If you’ve ever worked in industries like mining, quarrying, or heavy construction, you know abrasive environments aren’t just tough—they’re brutal on every piece of equipment you throw at them. Over the years, I’ve talked to so many guys on site who come back frustrated because their electrofusion fittings wore out way faster than they should. Last month, I even hopped on a call with a mine foreman who said he’d replaced 12 poly fittings in a single shift, all because the grit and dust in his site ate through the joints before they could even reach their first maintenance check. That’s when it hit me: most people don’t realize that installing electrofusion fittings in these harsh spaces isn’t just “bolt and go”—there are specific requirements you have to follow to keep leaks, failures, and downtime at bay. As a guy who’s been selling electrofusion fittings for 10+ years, I’ve seen what works and what doesn’t, and today I’m breaking down exactly what you need to know. Electrofusion Fittings
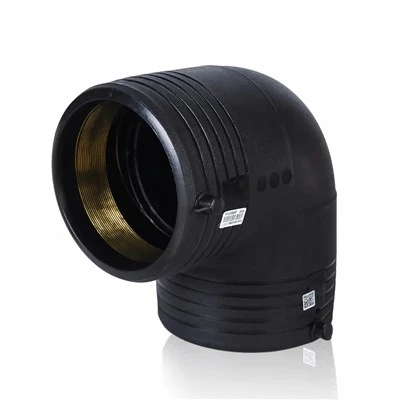
First off, let’s get one thing straight: abrasive environments aren’t just “dirty.” We’re talking about places where silica dust, coal fines, gravel, or metal shavings are floating around nonstop—particles so small they can sneak into the tiniest gaps, scratch surfaces, and wreck even the sturdiest joints. So, step one for installation? Stop treating the work surface like a job site you’d find in an office. I’ve watched new techs grab a random rag off the ground to wipe down a pipe end, only to realize that rag had a tiny piece of gravel tucked in the fold. That’s a quick way to ruin an electrofusion joint—even a tiny contaminant between the pipe and fitting stops the heat from bonding properly, leading to a weak spot that’ll fail when the abrasive dust gets into the system.
So, what’s the actual cleaning requirement here? It’s not just “wipe it off”—it’s mechanically clean the entire fusion zone. That means using a dual-action sander (not a random orbital, trust me—those can leave swirl marks that trap grit) or a dedicated pipe scouring pad made specifically for HDPE and poly pipes. I always tell my customers to sand at least 2 inches beyond where the fitting will sit on both sides. Once you’ve sanded, you can’t use a paper towel or a shop rag to wipe it—those leave micro-fibers. Instead, use lint-free non-woven wipes, and grab a small air compressor with a nozzle to blow every last bit of dust and debris out of the pipe end before you even touch the fitting. And here’s a pro tip I picked up from a pipeline guy in Australia: once you clean the pipe, cover the end with a plastic cap immediately. Even if you take a 5-minute break, that dust will find its way in. I can’t tell you how many times a customer will show me a pipe that was “cleaned 10 minutes ago” and blow a bunch of grit out when I check it. Don’t be that person.
Next up, the alignment of the pipe and fitting. In abrasive environments, this isn’t just about making a pretty joint—misalignment is a quick ticket to a failed fusion. Let’s be real: on busy job sites, pipe ends are often cut quickly with a hand saw, leaving them slightly off-square, or they get knocked out of alignment when you’re moving other equipment around. But when you’re fusing, if the pipe is even 1mm off-center inside the electrofusion fitting, the heat won’t distribute evenly. That means one side will be under-heated (weak bond) and the other side might even melt too much, leading to gaps where grit can get in later.
So, what’s the right way to align in these spaces? First, always use a straightedge to check the pipe end is square. If it’s cut at an angle, you need to trim it properly—don’t try to force it into the fitting, that’ll only cause problems. Then, use a dedicated alignment clamp, not whatever pipe wrench you have lying around. A lot of guys think clamps are a hassle, but in abrasive environments, they’re non-negotiable. I once had a customer skip the clamp to save 10 minutes, and three months later, a joint blew on a slurry line full of rock. The misalignment had created a tiny crack that the grit widened over time. The clamp keeps the pipe centered, so the electrofusion element inside the fitting heats evenly across the entire joint. Also, make sure there’s no gap between the pipe and the fitting collar. If there’s even a 0.5mm gap, grit can seep in during fusion or after, breaking the bond.
Then there’s the temperature factor. Abrasive environments are usually either super hot or freezing cold—think 100+ degrees in a quarry in Arizona, or below zero at a northern mine in the winter. Neither is great for electrofusion, but most people overlook how ambient temperature affects the installation. The electrofusion element inside the fitting is calibrated to heat at a specific rate, usually between 200 and 220 degrees Celsius, but that’s when the ambient temp is between 10 and 30 degrees Celsius. If it’s 40 degrees outside, the fitting will absorb more heat from the air, so it’ll take less time to reach the correct temp, leading to under-heated joints. If it’s 0 degrees, the opposite happens: the fitting loses heat faster, so you need to add extra time to the fusion cycle.
I always tell my customers to check the ambient temp before you start any fusion. Most modern electrofusion controllers have a setting for ambient temp, but a lot of guys just use the default setting out of the box. That’s a mistake. Last winter, I worked with a group in Manitoba who didn’t adjust for the -5 degree weather, and their joints failed 6 months early because the fusion was too weak. Also, if it’s raining or snowing, don’t even try to fuse outdoors. Moisture is another contaminant that ruins joints, and abrasive environments are already wet half the time (slurry lines, water lines for dust control). If you have to work in damp conditions, use a temporary shelter or a heat tent around the fitting to keep it dry during fusion. It’s an extra 15 minutes, but it beats replacing a line because of a bad joint.
Another big one: handling the fittings themselves. You’d be surprised how many people don’t think about what happens to the fitting before it even gets to the job site. In abrasive environments, electrofusion fittings can get beat up during transport—scratches on the outer collar, dust built up in the element slots, even tiny chips in the plastic. Those scratches might not look like a big deal, but when you put the clamp on, they can create pressure points that damage the fitting or lead to uneven heating. Also, dust in the element slots can cause a bad connection between the controller and the fitting, so the fusion cycle doesn’t run correctly.
So, how do you handle fittings right in these spaces? First, inspect every single fitting when it arrives, not just once. Check the outer surface for deep scratches or chips, and make sure the element slots are completely clean. If a fitting has a scratch deeper than 1mm, send it back—don’t risk using it. When you’re moving fittings around the job site, don’t just throw them in the back of a truck with shovels and gravel. I always recommend storing them in a dedicated plastic bin, not on the ground where grit can get in. And when you put the fitting on the pipe, don’t drag it across the ground—lift it, and if you have to move it along the pipe, slide it on gently, not roughly. Scratching the pipe or the fitting at this stage is a easy avoidable mistake that causes big problems later.
Now, let’s talk about post-installation checks. A lot of guys think once the fusion cycle is done, they’re good to go—but in abrasive environments, a quick check isn’t enough. You have to wait the full cooling time, too. Most electrofusion fittings need 1 to 2 hours of cooling time, depending on the size, but in abrasive conditions, that time is non-negotiable. If you move the pipe or apply pressure too early, the bond isn’t fully set, and grit can get into the joint. I once had a customer test a joint 30 minutes after fusion, because he was in a hurry to keep the line running, and the joint leaked. The cooling time is there for a reason—let the plastic solidify properly under the correct pressure from the clamp.
Also, after cooling, do a visual check and a pressure test. For the visual check, look for squeeze-out around the joint— that’s the excess melted plastic that comes out when the pipe and fitting fuse. Squeeze-out should be uniform all around the joint, no gaps or missing spots. If you notice uneven squeeze-out, that’s a sign the alignment was off or the heat was wrong. For the pressure test, don’t just test at regular operating pressure—add 20% more pressure for a short time to make sure the joint can hold. Abrasive environments put extra stress on joints, so testing above the normal pressure gives you a safety buffer.
Wait, one more thing: regular maintenance, not just installation. Even if you follow all these steps, abrasive dust will eventually catch up to your joints. So, every 3 to 6 months (depending on how harsh your environment is), do a visual check of all electrofusion fittings. Look for scratches on the outer collar, cracks, or dust building up around the joint. If you see any of that, clean the joint and do a quick pressure test. I know it’s a hassle, but it’s way better than a catastrophic line failure that shuts down your site for 8 hours.
At the end of the day, electrofusion fittings in abrasive environments aren’t rocket science, but they do require paying attention to the small details that most people skip. The extra 10 minutes you spend cleaning the pipe, checking alignment, adjusting the controller, and waiting for cooling time will save you hundreds, if not thousands, of dollars in downtime and replacement parts. If you’re working in a mining, quarry, or construction site, don’t cut corners on installation—those small mistakes add up fast.

If you have questions about which electrofusion fittings work best for your specific abrasive environment, or need tips for your next job, feel free to reach out. We’ve worked with dozens of teams in heavy industries to get their installations right, and we’re here to help you avoid those frustrating failures. Don’t wait until your next line leaks—let’s talk about how to set up your joints to last.
Electrofusion Fittings References:
ASTM F1290, Standard Practice for Electrofusion Joining of Polyethylene Pipe and Fittings for Gas Distribution, 2021
ISO 13953, Plastics piping systems for the conveyance of fluids – Polyethylene (PE) pipes and fittings – Electrofusion jointing, 2018
Mining Safety and Health Administration (MSHA), Guidelines for Pipeline Installation in Abrasive Mine Environments, 2022
Plastic Pipe Institute (PPI), Technical Report TR-42: Electrofusion Joining of HDPE Pipe in Harsh Operating Conditions, 2020
Yuyao Aoshi Hydraulic Components Manufacturing Co., Ltd.
As one of the most professional electrofusion fittings manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to wholesale electrofusion fittings in stock here and get quotation from our factory. Customized orders are welcome.
Address: Huilong village, Zhangting town, Yuyao city, Zhejiang province, China.
E-mail: renxuwei@vip.163.com
WebSite: https://www.jintongtrading.com/
