If you’ve ever stood in a machine shop watching a slant bed lathe carve precise parts out of solid metal, you might have wondered: how accurate is this thing, really? As someone who’s spent the last 12 years working with slant bed lathes as a supplier—talking to job shop owners, aerospace technicians, and custom fabricators every week—I can tell you accuracy isn’t just a number on a spec sheet. It’s a mix of design, setup, maintenance, and even the material you’re cutting. Let’s break this down without the jargon, because I know most of you reading this just need to get parts that fit, not decode engineering textbooks. Slant Bed Lathe
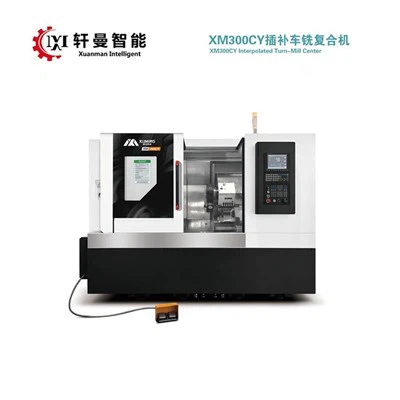
First, let’s get one thing straight: slant bed lathes are designed for accuracy, unlike their flat bed counterparts. The slant bed—usually a 30 or 45 degree incline—puts the Z-axis and X-axis slides at an angle that keeps chips and coolant from pooling on the ways. That might sound like a tiny design choice, but less debris on the ways means less friction, less wear, and more consistent movement. Early flat bed lathes had problems with swarf building up between the ways, which would cause the tool to drift even after just a few hours of operation. Slant beds solve that, right off the bat. But accuracy isn’t just about the bed shape—it’s about two key measurements: positional accuracy and repeatability. Positional accuracy is how close the lathe’s tool tip gets to where the CNC says it should be. Repeatability is how consistent that position is every time you tell it to move to the same spot. I’ve seen job shops turn out parts that are off by a thousandth of an inch (0.001 mm) with a worn flat bed, but a new slant bed lathe will hold 0.0005 inch (0.0127 mm) positional accuracy out of the box, and repeatability that’s even tighter—often 0.0002 inch (0.005 mm). That’s the difference between a part that bolts together on the first try and one that needs hours of rework.
Now, you might be asking: where do these numbers come from? When we build slant bed lathes, we test them using laser interferometers—no tape measures here, trust me. A laser beam bounces off a mirror attached to the tool, and the machine measures how far it moves with precision down to millionths of an inch. That’s not just our QC team playing around; that’s the industry standard set by organizations like the International Organization for Standardization (ISO) and the American Society of Mechanical Engineers (ASME). For a standard entry-level slant bed lathe, you’ll see accuracy specs like ±0.001 inch per foot in the Z-axis, and ±0.0008 inch in the X-axis. Mid-range models for small to medium production crank that down to ±0.0005 inch per foot, and high-precision models for aerospace or medical work hit ±0.0002 inch per foot. But here’s the catch: those specs are for the machine in a controlled environment—like our temperature-regulated factory floor, where humidity and temperature stay steady (most shops don’t have that luxury, I get it). Even a 10 degree F change in a shop floor can cause the metal ways to expand or contract, throwing accuracy off by a tiny bit. That’s why experienced operators will let the machine warm up for 30 minutes to an hour before running a production batch. It’s not just a myth; it’s a small step to keep those accuracy numbers on track.
What about common factors that throw accuracy off? I’ve had customers call me panicking because their brand-new slant bed lathe is cutting parts that are 0.003 inch off, and 9 times out of 10, it’s not the machine’s fault. First, setup. If you don’t level the lathe properly—even a tiny tilt of the bed can shift the axes as you move the tool—you’re going to get inaccurate cuts. I always tell customers to use a precision level on the ways and check it every few months, especially if the shop has heavy foot traffic or a forklift driving nearby (vibration from that will shift the machine too). Second, tooling. A worn insert or a tool holder that’s not clamped tight will make the tool tip drift. Last month, a customer blamed our lathe for bad fuel injector parts, and it turned out he was using a 10-year-old tool insert with a chipped cutting edge. Once he swapped it, the parts were spot on. Third, material variability. Soft aluminum might cut easily, but it can chatter if the feeds and speeds are off, leading to dimensional error. Hard steel will wear the ways faster if you’re not using the right lubricant, and over time, that wear will lower accuracy. Slant bed lathes are durable, but they’re not unbreakable—proper maintenance goes a long way.
Let’s talk about real-world examples, because specs mean nothing if you can’t see them in action. Last year, we sold a 15-inch slant bed lathe to a custom aerospace parts shop in Texas. They were making turbine blades that needed to fit within 0.002 inch of the blueprint—any more, and the engine wouldn’t pass inspection. Their old flat bed lathe was getting 0.004 inch variance on the Z-axis, so they were spending $200 an hour reworking parts. After installing the slant bed lathe, we programmed a test run of 5 blades. The average variance was 0.0004 inch. They cut their rework time by 75% and increased production by 20% because the machine was running faster without sacrificing accuracy. That’s the payoff right there. Another example: a medical device shop that makes small bone screws. Those screws need threads that are uniform within 0.001 mm—way tighter than what a flat bed can hold. Their slant bed lathe was holding that consistency for 10,000 parts in a run, with only one out of spec. That’s the kind of accuracy that turns a good machine into a profit center.
Wait, but what about entry-level slant bed lathes vs. high-end ones? I get that not every shop needs aerospace precision. Our entry-level slant bed lathes are built for small to medium job shops, hobbyist run production, and general machining. They have the same slant bed design, so they hold better accuracy than flat beds, but their linear slides are precision ground instead of super precision, so their accuracy is around ±0.002 inch per foot. That’s more than enough for parts like furniture hardware, engine brackets, or farm equipment components. The mid-range models add pre-tensioned ball screws and higher grade linear guides, so accuracy jumps to ±0.0005 inch per foot—perfect for automotive parts, custom valves, and general prototype work. Our high-precision line uses linear motors instead of ball screws (no wear, no backlash) and has temperature compensation built in, so accuracy hits ±0.0002 inch per foot. Those are the ones for aerospace, medical, and defense parts where even a tiny error can be catastrophic. It’s not that one is “better”—it’s matching the machine’s accuracy to your actual needs. Buying a $50,000 high-precision lathe for making door knobs is a waste of money, just like using a $20,000 entry-level slant bed for turbine blades is going to get you into trouble.
Another thing I should mention: backlash. Backlash is the tiny gap between the gear teeth or screw threads that makes the tool move a little when you reverse direction. That’s a big enemy of accuracy, especially when you’re cutting threads or making parts that require multiple passes. Slant bed lathes with ball screws have very minimal backlash—usually less than 0.0005 inch—and our premium models have backlash compensation built into the CNC, so the machine automatically adjusts for that gap. Flat bed lathes often have more backlash because their way systems are older design, requiring more maintenance to keep that gap small. I’ve had customers ask me if they can fix backlash on an old flat bed, and yes, you can shim the ways or replace gears, but it’s never going to be as consistent as a slant bed’s factory-built minimal backlash.
So, what’s the takeaway for anyone looking at a slant bed lathe’s accuracy? It’s not a single number—it’s a combination of design, quality components, setup, maintenance, and your own operating practices. A good slant bed lathe will outperform a comparably priced flat bed on accuracy, period. But to get the most out of it, you need to invest in proper setup, routine maintenance (like lubricating the ways, checking for tight fasteners, and calibrating the laser every year or so), and matching the machine to your part requirements. I’ve seen too many customers buy a cheap slant bed lathe from a no-name brand, skip the setup, and then complain that it’s not accurate. The machines we sell are built with high-grade materials, tested before they leave our facility, and backed by our support team—we walk you through setup, offer training, and are on call if you run into issues.

At the end of the day, accuracy in a lathe isn’t about impressing other machinists with a tiny number—it’s about making parts that work, on time, without wasting material or labor. For job shops, that means more profits. For production shops, that means higher output. For critical industries, that means safer, more reliable products. If you’re in the market for a slant bed lathe and want to talk through what accuracy you actually need for your parts, feel free to reach out to our team. We don’t push the most expensive model—we help you pick the one that fits your production needs and budget, because your success is our success.
Five-axis Machining Center References
- International Organization for Standardization. (2019). ISO 230-2: Test code for machine tools – Part 2: Determination of accuracy and repeatability of positioning numerically controlled axes.
- American Society of Mechanical Engineers. (2021). ASME B5.54: Methods for performance evaluation of numerically controlled machine tools.
- Machine Builders Association. (2022). Slant bed lathe design principles for dimensional accuracy in precision machining applications.
- Aerospace Industries Association. (2020). Precision machining requirements for turbine component manufacturing.
Jiangsu Xuanman Intelligent Equipment Co., Ltd.
We’re well-known as one of the leading slant bed lathe manufacturers in China, featured by quality products and low price. Please rest assured to buy discount slant bed lathe made in China here from our factory. We also accept customized orders.
Address: No. 1-1, Weier Road, Jieji Equipment Manufacturing Industrial Park, Sihong County, Suqian City, Jiangsu Province, China
E-mail: jsxmzn@163.com
WebSite: https://www.xm-cnc.com/
